Guardian Solutions Plus
Financing Guardian Shield
Water splashing against a backdrop of the American flag

Manufacturing & Industrial Water Treatment Systems

Pure process water. Optimized production. Equipment reliability.

Commercial Water Treatment

Service By Industry

Manufacturing plants and industrial facilities depend on water quality directly affecting product quality, equipment performance, and operational efficiency. Paper mills require soft water preventing scale buildup in digesters and recovery boilers; food and beverage processors need microorganism-free water for product safety and shelf life; electronics manufacturers demand ultra-pure water free of minerals and particulates affecting product performance; metal finishing operations require deionized water preventing corrosion and ensuring coating quality; chemical plants need process water meeting strict purity specifications; textile operations depend on consistent water chemistry for dye consistency and fabric quality.

Guardian Solutions Plus designs and installs industrial-scale water treatment systems engineered for manufacturing environments. We conduct facility water audits, test source water identifying contaminants affecting production, recommend treatment solutions optimizing both water quality and operational cost, handle professional installation integrated with production schedules, and provide ongoing maintenance that helps prevent downtime and protects capital equipment.

Using Lancaster Water Group X-Factor commercial systems scaled for industrial demand and backed by 40+ years of manufacturing water expertise, we deliver treatment systems that enhance production quality, extend equipment life, and optimize your manufacturing water investment.

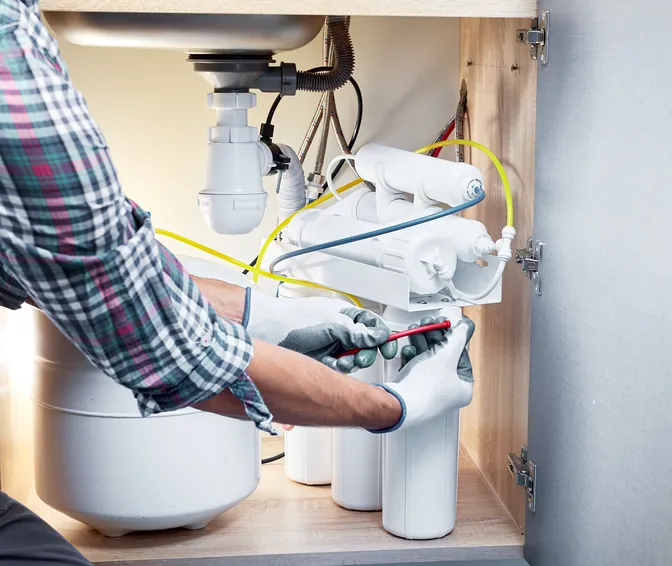
A Guardian Solutions Plus technician servicing an industrial water treatment system
Check your monthly payment options with Hearth financing (opens in a new tab)

Why It Matters

Why Manufacturing & Industrial Operations Choose Professional Water Treatment

  • Production Quality & Product Specification Compliance

    Manufacturing processes depend on water chemistry directly affecting finished product quality. Paper mills require soft water preventing scale and color variation in pulp processing; food and beverage operations need microorganism-free water ensuring product safety and preventing spoilage affecting shelf life and customer satisfaction; electronics fabrication demands ultra-pure water free of particles and minerals that contaminate circuits and reduce yield; textile operations need consistent pH and mineral content ensuring dye uptake and fabric color uniformity; chemical plants require process water meeting strict purity specifications for reagent effectiveness and batch consistency; metal finishing requires deionized water preventing contamination-driven finish defects and rework. Hard water, bacterial contamination, mineral-laden supply, or chemical contaminants introduce product defects, increase rework and waste, reduce yield, and trigger customer quality complaints. Professional water treatment ensures process water consistently meets your production specifications, eliminating water-quality-driven yield loss and rework.

  • Equipment Protection & Operational Longevity

    Water quality directly impacts equipment performance and maintenance costs in industrial settings. Scale buildup on boiler tubes, heat exchangers, and recovery systems reduces thermal efficiency and forces emergency cleaning or replacement; bacterial biofilm in cooling systems reduces heat transfer efficiency and increases biological corrosion; mineral deposits on pump impellers and nozzles cause cavitation damage and premature failure; chlorine residue corrodes stainless steel components and accelerates metallic corrosion in sensitive processes; suspended solids damage high-precision equipment and plug filtration systems. Professional water treatment removes scale-forming minerals, bacterial contamination, chemical residues, and particulates, protecting capital equipment from corrosive and scale-related failure modes. Equipment protected by properly treated water operates reliably, requires fewer emergency repairs, and reaches or exceeds its designed operational lifespan.

  • Energy Efficiency & Operational Cost Optimization

    Water quality directly impacts energy consumption and operating costs in industrial processes. Hard water-induced scale on boiler tubes, heat exchanger surfaces, and condenser tubes increases energy consumption—a quarter-inch of scale can increase fuel consumption 10-12%; bacterial biofilm in cooling systems reduces heat transfer efficiency requiring higher flow rates to maintain temperature control; mineral deposits restrict flow increasing pump head and reducing efficiency; low-pH corrosive water requires additional corrosion inhibitor chemicals increasing chemical treatment costs. Soft water, deionized water, and properly conditioned process water reduce scale formation, improve heat transfer, reduce flow restrictions, and lower chemical treatment needs. Professional water treatment reduces energy consumption, decreases chemical costs, and improves overall operational efficiency—benefits that often pay for treatment systems through operational savings within months.

  • Regulatory Compliance & Environmental Protection

    Industrial water discharge is heavily regulated. Manufacturing facilities must comply with EPA Clean Water Act regulations, state environmental requirements, and local water authority discharge standards limiting the contaminants, temperature, and chemistry of water returned to municipal systems or surface waters. Failure to meet discharge standards triggers violations, fines, operational restrictions, or forced facility shutdowns. Professional water treatment ensures your discharge water meets regulatory standards, reduces environmental impact of your operations, and protects your facility from compliance violations. Industries with advanced water treatment systems can often discharge to standards others cannot meet, creating competitive advantage in regulated markets.

  • Downtime Prevention & Production Continuity

    Water system failures in manufacturing aren’t inconveniences—they halt production and cost thousands per hour in lost output, rework, and customer impact. A cooling system failure shuts down production; a boiler scale-induced rupture creates emergency repair urgency; contamination of process water requires batch rework; equipment failures prevent scheduled shipments. Properly designed water treatment systems prevent the contamination, scale, and corrosion that cause failures. We design systems with redundancy so maintenance doesn’t halt production, establish preventive maintenance protocols catching problems before they escalate, and back every installation with dependable technical support. Most production interruptions are prevented through proactive treatment system monitoring and maintenance.

  • Process Optimization & Throughput Improvement

    Manufacturing output depends on process conditions including water quality, temperature, and chemistry. Soft water, deionized water, and properly pH-adjusted process water allow operations to run at design capacity; hard water forces operators to reduce flow or throughput to prevent scale; contamination requires batch quarantine and rework; equipment inefficiency reduces production speed. Well-designed water treatment systems enable operations to run at full design capacity, eliminate water-quality-driven production slowdowns, reduce downtime for cleaning or maintenance, and improve overall throughput. Some customers find professional water treatment increases effective production capacity without capital equipment investment.

  • 40+ Years of Manufacturing & Industrial Water Expertise

    Guardian Solutions Plus is a manufacturing water specialist, not a residential contractor applying home techniques to industrial operations. Backed by four decades of water treatment experience, we design and install systems for paper mills, food and beverage producers, electronics manufacturers, metal finishing operations, chemical plants, textile mills, and other industrial operations across Pennsylvania. We understand production constraints, equipment specifications, regulatory compliance requirements, and the non-negotiable nature of water quality in manufacturing environments. Our manufacturing experience means we approach every facility with production discipline and operational awareness.
Your Options

Water Treatment Systems for Manufacturing & Industrial Operations

Manufacturing facilities operate under unique water-quality demands based on specific processes, equipment specifications, source water characteristics, and regulatory requirements. Groundwater-fed mills face iron, manganese, and hardness challenges; municipal-water users need chlorine and chlorine-byproduct removal; facilities near industrial areas may face emerging contaminants; all manufacturing operations benefit from water quality optimization reducing equipment stress and improving process consistency. We conduct comprehensive facility water audits identifying water-quality issues affecting your processes, test source water revealing contaminants and mineral content impacting your operations, understand your equipment specifications and process requirements, and design customized treatment addressing contamination while optimizing operational efficiency and cost.

Treatment combinations depend on your manufacturing processes. Paper mills and boiler operations need soft water preventing scale; food and beverage processors need deionized water ensuring product purity; electronics manufacturers need ultra-pure water free of particles and minerals; cooling systems need corrosion inhibition and biofilm prevention; chemical processes need water meeting strict purity and pH specifications. Scalable systems layer treatment—removing sediment, hardness, bacteria, minerals, and chemical contaminants in sequence—so your facility gets reliably pure process water optimized for your manufacturing specifications.

We Have a Solution for That! Contact Our Team Here

Our Process

Manufacturing & Industrial Water System Implementation

Before designing any system, we understand your facility’s specific manufacturing processes, water uses, equipment specifications, and operational constraints. We conduct a comprehensive facility audit identifying all water-use points (boilers, cooling systems, process equipment, cleaning), assess current water treatment if any, understand your equipment manufacturers’ water-quality requirements, review applicable regulatory and discharge standards, and identify seasonal variations or source-water challenges specific to your operation. This assessment becomes the foundation for treatment design.

  • Conduct facility walkthrough mapping all water-use locations and operational processes
  • Identify water-use volumes and peak demand patterns for each process
  • Review equipment manufacturers’ water-quality specifications and recommendations
  • Assess current water treatment systems and identify performance gaps
  • Collect baseline water samples from source entry point and process-use locations
  • Determine regulatory compliance requirements and environmental discharge standards
  • Identify production constraints and maintenance windows available for system work

We conduct industrial-scale water testing revealing minerals, hardness, bacteria, chemical contaminants, particulates, pH, and other parameters affecting your manufacturing processes and equipment. Testing includes mineral and hardness analysis affecting scaling potential; bacterial and microbial analysis affecting product safety and cooling system performance; chemical contaminant detection (chlorine, chlorine byproducts, fluoride); particulate analysis affecting precision equipment; and corrosivity assessment affecting equipment longevity. Test results guide treatment design and become your baseline for measuring treatment system performance.

  • Analyze mineral content, hardness, and scaling potential in your water source
  • Conduct bacterial and microbial analysis affecting process water and cooling systems
  • Test for chemical contaminants including chlorine residue and industrial byproducts
  • Measure particulate matter and turbidity affecting equipment and product quality
  • Assess pH, alkalinity, and corrosivity affecting equipment protection and chemical control
  • Identify contaminants specific to your water source and geographic region
  • Document findings with technical reporting supporting treatment system design

Based on testing, facility review, and process requirements, we design an industrial-scale water treatment system engineered for your specific manufacturing applications and operational constraints. We select treatment technologies matched to your contamination profile and purity requirements (softening, deionization, reverse osmosis, filtration, UV disinfection), size systems for your facility’s peak process demand with surge capacity, plan system integration minimizing production disruption, establish monitoring and maintenance protocols preventing performance drift, and document system specifications meeting your equipment and process requirements.

  • Specify treatment stages addressing contamination identified in testing
  • Select industrial-scale equipment validated for manufacturing applications
  • Design system configuration optimizing both water quality and operational cost
  • Size equipment for peak process demand plus seasonal variation
  • Plan system location and infrastructure integration with production schedules
  • Establish water-quality monitoring and performance testing protocols
  • Create maintenance and media replacement schedules preventing downtime
  • Document system specifications and performance warranties

We install systems integrating seamlessly with ongoing manufacturing operations and scheduled around production windows. We coordinate timing with facility operations, plan system location and piping routing minimizing production impact, manage all permits and regulatory notifications, commission systems with full performance testing confirming water quality meets specifications before production use. Professional installation includes redundancy so system maintenance doesn’t halt production.

  • Coordinate installation timing around production schedules and maintenance windows
  • Obtain required plumbing permits and regulatory notifications for industrial water systems
  • Install treatment system at optimal facility location with proper infrastructure
  • Connect all water lines with industrial-grade materials matching equipment specifications
  • Install isolation valves, bypass systems, and redundancy enabling maintenance without shutdown
  • Conduct pressure, performance, and safety testing on all connections
  • Verify system performance meets documented water-quality specifications
  • Commission system with full operational verification before production use

Installation is complete when your operations team understands system operation, maintenance protocols, monitoring procedures, and when to contact us for support. We establish ongoing water-quality testing and equipment monitoring, create preventive maintenance schedules, optimize chemical treatment and operational parameters based on performance data, and provide dependable ongoing technical support. We monitor system performance continuously, conduct regular water-quality testing, schedule proactive equipment maintenance, and maintain performance documentation supporting your operational records.

  • Train operations and maintenance staff on system operation and monitoring
  • Provide written operation, maintenance, contingency, and troubleshooting protocols
  • Establish water-quality testing schedule with documented results and trend tracking
  • Set up automated monitoring confirming system performance against specifications
  • Create equipment maintenance reminder system ensuring timely media and filter replacement
  • Monitor energy efficiency and optimize operational settings for cost reduction
  • Develop contingency procedures for system issues or contamination
  • Schedule regular follow-up inspections, performance audits, and equipment validation

Financing Options

Flexible Financing for Water Treatment & Air Quality Systems

A new water treatment or indoor air quality system is an investment in your Green Lane-area home, and Guardian Solutions Plus offers flexible financing through Hearth to help make that investment manageable. Rather than putting off a repair or upgrade your home needs, Hearth’s financing options let you move forward now and pay over time. Get started today and see your personalized payment plans without affecting your credit score.

Hearth makes it easy for you to find monthly payment options for your project, with:

  • Hearth
  • Loan amounts up to $250,000

  • Affordable monthly payment options

  • Funding within 1-3 days

  • No Prepayment Penalties

  • No Home Equity Required

Our Guardian Shield Maintenance Agreement

Guardian Shield Maintenance Agreement

Regular maintenance is what keeps a water treatment or air quality system performing the way it’s supposed to, whether it’s protecting a Green Lane household or keeping a commercial facility compliant. Guardian Solutions Plus offers maintenance plans for both residential and commercial customers.

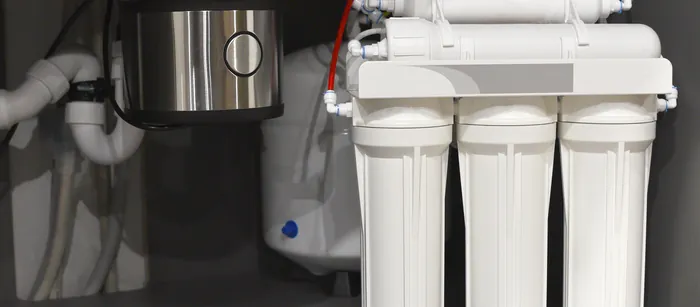
An under-sink reverse osmosis filter bank installed beside a kitchen disposal

Residential Guardian Shield Maintenance Agreement

  • Scheduled system check-ups for water softeners, filtration, and RO systems
  • Water testing to catch changes in water quality before they become a problem
  • Priority scheduling for households enrolled in a maintenance plan
  • Peace of mind knowing your system is being looked after by the same team that installed it
Learn More About the Guardian Shield Maintenance Agreement
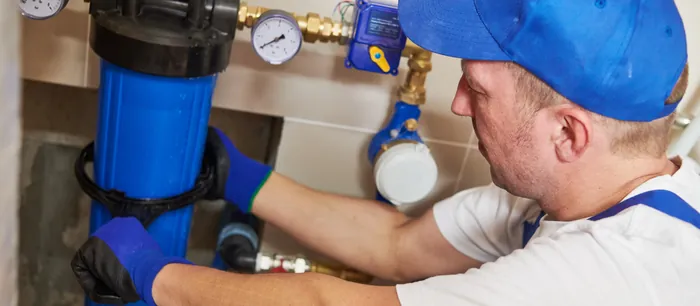
A technician servicing a commercial water filter housing fitted with pressure gauges

Commercial Guardian Shield Maintenance Agreement

  • Scheduled maintenance visits tailored to your facility’s water treatment demands
  • Testing and monitoring to help support regulatory and quality requirements
  • Reduced risk of unplanned downtime from equipment failure
  • A dedicated point of contact for ongoing commercial service needs
Learn More About the Guardian Shield Maintenance Agreement

Warranty Available on System Install

Every system we install is built to last — and backed to match. Guardian Solutions Plus offers a 10-year parts and labor warranty on new system installations, so both the equipment and the workmanship behind it are covered for a full decade. That means no surprise repair bills and complete peace of mind long after the install is done.

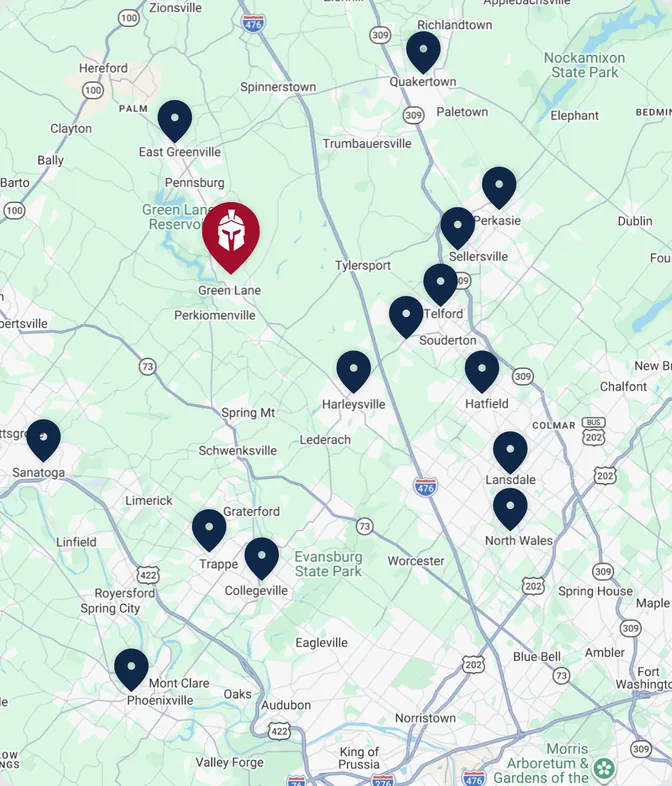
Map of the Guardian Solutions Plus service area across Montgomery and Bucks County, Pennsylvania

Service Areas

Manufacturing & Industrial Water Treatment Throughout Pennsylvania

We serve manufacturing facilities and industrial operations across Pennsylvania with professional water treatment expertise and production-focused support.

Additional Communities Served

We serve communities across Bucks and Montgomery Counties, and we’re often working in towns just beyond our core service area. Check your location or call us — we’ll let you know how soon we can help.

Frequent Questions

Manufacturing & Industrial Water Treatment Questions

  • Family Owned & Operated

  • Backed by 40+ Years of Experience

  • Certified WQA Members

  • Trusted Brands

  • Residential & Commercial Services

Taste the Difference

Optimize Manufacturing Efficiency With Professional Industrial Water Treatment

Manufacturing operations depend on water quality directly affecting product quality, equipment performance, and operational cost. Poor water quality forces production slowdowns, increases equipment maintenance and downtime, reduces product yield, increases rework, and raises operational expenses. A quarter-inch of scale on boiler tubes increases energy consumption 10-12%; bacterial biofilm reduces cooling efficiency; suspended solids damage precision equipment; hard water requires additional chemical treatment. Guardian Solutions Plus brings 40+ years of manufacturing water expertise and Lancaster X-Factor industrial systems engineered for production environments and operational efficiency.

We handle the complete process: comprehensive facility water audits revealing contamination and inefficiencies affecting your operations; professional testing identifying minerals, bacteria, chemicals, and particulates impacting process quality and equipment performance; custom system design engineered for your specific manufacturing applications and regulatory requirements; professional installation integrated with production schedules and minimal operational disruption; and ongoing support with regular testing, preventive maintenance, and performance optimization keeping your operations running efficiently.

Professional water treatment directly improves manufacturing profitability: soft water reduces energy consumption and chemical costs; deionized water improves product quality reducing rework; corrosion control extends equipment life and reduces maintenance; proper treatment enables production at design capacity improving throughput. Every dollar invested in industrial water treatment returns through improved efficiency, extended equipment life, reduced downtime, and better product quality. Review the full Commercial Water Treatment overview to compare treatment trains, and consider point-of-entry and point-of-use systems that combine facility-wide treatment with process-specific polishing for precision equipment.

Plant managers can fund system upgrades with flexible financing through Hearth, sustain performance with a commercial maintenance plan, review current specials and rebates, and learn about Guardian Solutions Plus and four decades of industrial water experience.

Two whole-home water softener and filtration tanks installed in a basement